Achieving consistent packaging quality begins with understanding how to ensure wall thickness uniformity in packaging molds. Uneven walls can create weak corners, sink marks, warping, or unpredictable cooling. A container may look acceptable outside while its inner wall remains dangerously thin. The result? Higher rejection rates.
In practical mold development, engineers study the part design before cutting steel. They check draft angles, corner radii, gate location, flow length, and expected shrinkage. Material selection matters too. Different polymers respond differently to pressure, temperature, and cooling time. A small change in melt temperature can affect a thin neck or handle section. Small errors matter. Moldflow analysis can reveal likely imbalance, but simulation is not a substitute for physical testing.
Reliable control combines design review, process monitoring, and dimensional inspection. Engineers should measure wall sections at several heights and around the full circumference. Ultrasonic gauges, sectioned samples, and coordinate measuring equipment can expose variations that visual checks miss. Cooling channels also deserve close attention, especially near thick bases and narrow corners. Inconsistent cooling often explains distortion after ejection. However, no method is perfect. Real production conditions may differ from laboratory trials, and operators may adjust settings under pressure. That reality needs to be documented, not ignored. A robust approach compares trial data with production measurements, records corrective actions, and reviews results against applicable quality requirements. This disciplined feedback helps packaging manufacturers improve mold reliability, reduce material waste, and deliver containers with dependable performance.
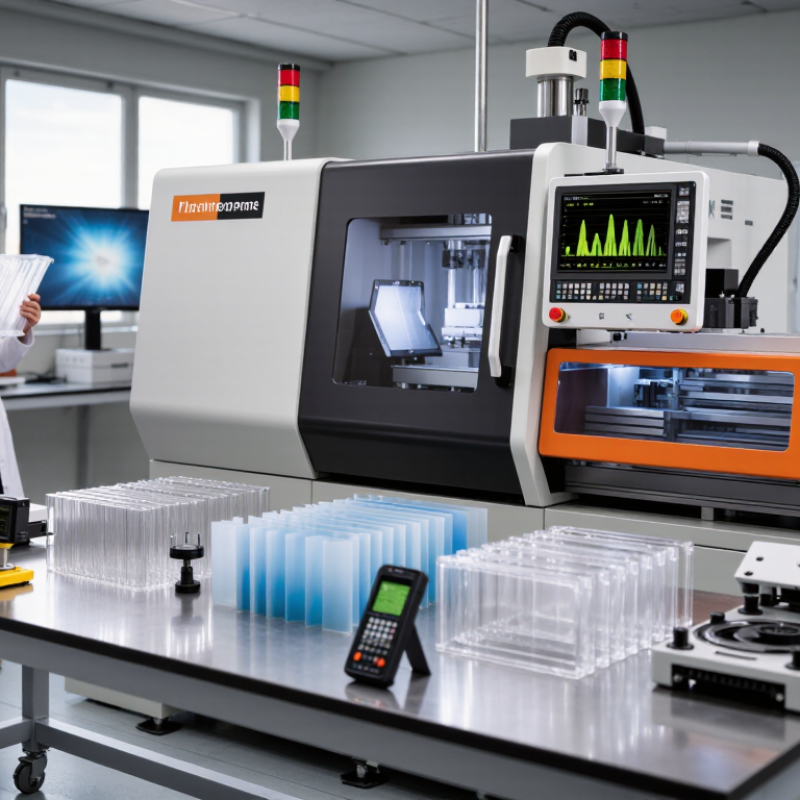
Wall thickness variation usually begins with uneven polymer flow. Gate position, runner balance, and melt temperature strongly influence filling behavior. A long flow path may cool before the cavity is full. Thin areas then appear near the end of filling. Thick areas often form around gates, corners, or ribs. I have seen a small gate offset create visible panel distortion after ejection.
Cooling is another major cause. Unequal channel spacing leaves one mold surface hotter than the other. The hotter side cools later and shrinks differently. Mold temperature differences of only a few degrees can matter. Poor venting can also trap air and restrict local packing. The result is inconsistent density, gloss, and wall measurement. Not every defect comes from the machine.
PlasticsEurope and EPRO reported that packaging represented 39.5% of European plastics demand in 2022. That scale makes small process variations costly. Industry injection-molding studies commonly identify holding pressure, cooling time, and material shrinkage as key dimensional factors. These variables must be checked together, not separately. Operators should measure parts at several points, including corners and gate zones. A simple 3D scan may reveal patterns that calipers miss. CAD assumptions can be wrong. Real production data should challenge them.
How to Ensure Wall Thickness Uniformity in Packaging Molds?
Designing Mold Geometry for Consistent Wall Thickness
Consistent wall thickness begins with balanced mold geometry, not machine settings alone. A thin corner cools quickly, while a thick base retains heat and shrinks later. This difference can create sink marks, warpage, or weak seals. During mold trials, measure several points around the container, including ribs, shoulders, and gate areas. A practical target is often a variation below 5% for demanding packaging parts, although the final tolerance depends on resin, shape, and function.
Smithers’ report, The Future of Global Packaging to 2028, forecasts the packaging market will approach 1.2 trillion dollars by 2028. That growth increases pressure to reduce material without sacrificing strength. Designers can support this goal with gradual transitions, uniform radii, and ribs that remain thinner than the nominal wall. Avoid sudden thickness changes near the gate. They can redirect flow and trap air. I have seen small geometry changes improve filling, but not every result repeats perfectly. Mold design still requires testing.
Tips: Use flow simulation before cutting steel. Check the thinnest section first. Keep core and cavity cooling channels close to high-load areas. Use inspection data from at least three molded shots, not one sample. Remember that a beautiful CAD model may still hide uneven cooling. Reflect on the measurements, then revise the geometry.
Uniform wall thickness begins with material selection, not only mold geometry. In production trials, I compare melt flow, shrinkage, stiffness, and moisture sensitivity before approving a resin. A material that flows too easily may fill thin areas quickly, yet it can amplify local thinning near gates. One that resists flow may require higher pressure, increasing stress and uneven shrinkage. Small differences matter.
Processing conditions must match the chosen material and container design. Set melt temperature within the supplier’s validated range, then confirm it at the nozzle and cavity entrance. Mold temperature controls cooling speed, so cold spots can freeze one region while another remains fluid. I monitor injection speed, hold pressure, and cooling time using logged machine data. A short hold period often leaves the base underpacked, while excessive pressure can distort the shoulder. Use a designed experiment when possible, rather than changing three settings at once.
For verification, I section sample containers at the neck, shoulder, body, and base. Ultrasonic readings help, but calibrated cut-and-measure checks reveal gradients that sensors may miss. The first trial is rarely perfect. I have seen a stable average hide a thin corner only two millimeters wide. That finding changed the gate balance and cooling layout, although the adjustment increased cycle time slightly. This trade-off deserves review against drop performance, appearance, and dimensional limits. Keep records of resin moisture, barrel temperatures, cavity pressure, and measured thickness for every trial.
Wall thickness uniformity is controlled on the production floor, not only in mold design. Start with a stable melt temperature and verify it at the nozzle, not just on the controller. A 5°C difference can change viscosity and filling behavior noticeably. PlasticsEurope reported 400.3 million tonnes of global plastics production in 2022, showing the scale of process consistency required across packaging lines.
Set injection speed in stages. Use a slower profile near the gate to reduce jetting, then increase speed through thin sections. Monitor cavity pressure, screw position, and transfer timing for every shift. The U.S. Department of Energy identifies injection molding as an energy-intensive process, with typical energy use often ranging from about 0.9 to 2.5 kWh per kilogram. Unstable heating can therefore create both thickness variation and unnecessary energy loss.
Cooling time deserves equal attention. Uneven mold temperatures can leave one side soft while the other side has already contracted. Measure water temperature at both inlet and outlet. Check molded parts at several locations with a calibrated thickness gauge. In our trials, reducing cooling time initially improved output, but later caused warped bases. That assumption failed. ISO 294-1 also reminds processors to control conditioning before comparing test results. Record material moisture, melt temperature, cushion, and cycle time. Small drift becomes visible quickly.ores
| Process Stage | Key Parameter | Typical Production Target | Recommended Control | Effect on Wall Thickness | Corrective Action |
|---|---|---|---|---|---|
| Material Preparation | Resin moisture content | Within the resin supplier's specified limit; commonly below 0.02% for moisture-sensitive engineering resins | Measure with a moisture analyzer before processing and after extended hopper exposure | Excess moisture can cause splay, bubbles, reduced melt strength, and local thickness variation | Dry the resin using the validated time and temperature for the material; keep the hopper covered |
| Material Preparation | Regrind content | Use a controlled percentage established by product validation; maintain a consistent blend ratio | Verify the virgin-to-regrind ratio at every material change and production shift | Inconsistent regrind can change viscosity, shrinkage, and filling behavior | Standardize regrind particle size and blend ratio; segregate contaminated or thermally degraded material |
| Plasticizing | Melt temperature | Operate within the material's validated processing window, typically near the middle of the recommended range | Check actual melt temperature with a calibrated probe, not only the barrel setpoint | A melt that is too cold may freeze early; an overheated melt may flash, degrade, or shrink unevenly | Adjust barrel zones gradually and confirm the measured melt temperature after stabilization |
| Plasticizing | Screw recovery speed | Use the lowest speed that achieves the required recovery time without excessive shear heating | Trend recovery time, melt temperature, and screw speed together | Excessive shear may alter viscosity and create inconsistent filling from shot to shot | Reduce screw speed or back pressure if the measured melt temperature rises above the validated window |
| Plasticizing | Back pressure | Use a stable, validated setting sufficient for melt homogenization without unnecessary shear | Monitor pressure and recovery time for drift during the run | Too little back pressure may cause poor mixing; too much may increase melt temperature and shrinkage variation | Make small adjustments and verify part weight, melt temperature, and dimensional results |
| Filling | Injection speed profile | Use a repeatable multi-stage profile matched to the flow path and gate design | Record actual velocity and pressure curves for every validated mold setup | Unbalanced speed can cause premature freezing, jetting, hesitation, or uneven packing across the cavity | Increase speed before freeze-off in thin sections; reduce speed near the gate or at flow-front transitions when defects occur |
| Filling | Transfer position from fill to pack | Transfer consistently before the cavity is fully packed; validate using short-shot and pressure studies | Use screw position, cavity pressure, or a combined transfer method | Late transfer may cause flash and overpacking; early transfer may leave thin areas and sink marks | Adjust transfer position in small increments and compare cavity pressure, part weight, and thickness data |
| Packing | Holding pressure | Set high enough to compensate for volumetric shrinkage without causing flash or excessive residual stress | Use a documented pressure profile and monitor peak cavity pressure when available | Insufficient pressure can produce localized shrinkage; excessive pressure may distort thin walls or create flash | Increase pressure for confirmed sink or low-weight conditions; reduce it when flash or stress is detected |
| Packing | Holding time | Continue packing until the gate has sufficiently frozen; determine the setting with a part-weight study | Increase holding time stepwise and identify the point where part weight becomes stable | Short holding time causes under-packing; excessive time adds cycle time without improving thickness | Use the stable part-weight point as the initial production setting, then verify dimensions after cooling |
| Cooling | Mold temperature balance | Maintain the validated mold-temperature range and keep core and cavity sides balanced | Measure supply and return temperatures on each circuit; check for blocked channels | Uneven cooling causes differential shrinkage, warpage, and side-to-side wall variation | Balance cooling circuits, remove restrictions, and verify temperature uniformity across the mold |
| Cooling | Cooling time | Long enough for the part to maintain its shape after ejection; confirm through dimensional stability checks | Track ejection temperature and measure parts after a defined conditioning period | Early ejection can cause deformation and apparent thickness differences during handling or stacking | Increase cooling time or improve cooling efficiency if dimensions change after ejection |
| Mold Condition | Gate and vent condition | Keep gates free from wear and vents clean, with vent dimensions maintained within the mold design specification | Inspect during preventive maintenance and compare filling pressure trends | Restricted gates or vents can create hesitation, trapped gas, burn marks, and uneven filling | Clean vents, repair worn gates, and confirm the filling profile after maintenance |
| Production Control | Part weight | Maintain the validated nominal weight and control limits for the specific package design | Sample at start-up, after adjustments, and at defined intervals during production | Weight drift is an early indicator of changes in filling, packing, leakage, or material consistency | Stop and investigate when weight trends move toward control limits; do not compensate without identifying the cause |
| Production Control | Wall-thickness measurement | Meet the drawing tolerance and maintain the required minimum wall at all critical locations | Measure defined cross-sections using calibrated ultrasonic, optical, or destructive methods as appropriate | Directly confirms whether process adjustments are producing a uniform wall rather than only improving appearance | Map thin and thick zones, then correlate the results with gate location, cooling balance, and pressure history |
| Quality Release | Process data and first-off approval | Release production only after temperature, pressure, cycle time, weight, and thickness results meet approved limits | Use a standardized start-up checklist and retain traceable process records | Prevents unverified parameter changes from allowing non-uniform parts into the production batch | Quarantine parts made after uncontrolled deviations until dimensional and visual checks are completed |
Wall thickness uniformity starts with reliable inspection data, not visual judgment alone. In packaging molds, measure parts at fixed locations across every cavity. Use ultrasonic gauges for quick checks and cross-section analysis for verification. Record wall readings with cavity number, molding cycle, resin lot, and machine settings. This creates traceable evidence instead of isolated numbers. A 0.05 mm variation may seem minor, but it can affect stiffness, cooling time, and material use.
Quality teams should map thin and thick zones against mold geometry. Compare the data with gate position, cooling-channel layout, fill speed, and holding pressure. Statistical process control can reveal gradual drift before defects become obvious. When a cavity repeatedly produces thin walls, adjust steel dimensions or rebalance flow carefully. Do not change several variables at once. Otherwise, the result becomes difficult to trust. Data helps, but it is not innocent; poor sampling can lead to confident mistakes. Inspect the measurement method, too.
Tips: Measure warm and cooled parts separately. Calibrate instruments before each study. Check at least three parts per cavity. Use a simple color map to display thickness trends. Review rejected samples beside accepted parts. Keep one unchanged process setting as a reference. A practical target is not always the thinnest possible wall. It is a stable wall that meets performance needs with controlled variation. Some molds will need another trial. That is normal.
A thin corner cools quickly, while a thick base retains heat and shrinks later. Balanced geometry reduces sink marks, warpage, and weak seals. Machine settings cannot fix every geometry problem.
Demanding packaging parts often target variation below 5%. The final tolerance depends on resin, shape, and function. This target is useful, but not universal.
Use gradual transitions, uniform radii, and ribs thinner than the nominal wall. Avoid sudden thickness changes near the gate. Flow may redirect there.
Keep core and cavity channels close to high-load areas. Inspect corners, shoulders, ribs, and bases carefully. Cooling may look balanced in CAD, but behave differently in production.
Compare melt flow, shrinkage, stiffness, and moisture sensitivity before approval. Confirm melt temperature near the nozzle and cavity entrance. Track injection speed, holding pressure, and cooling time.
Short holding may leave the base underpacked. Excessive pressure can distort the shoulder. Insufficient cooling may increase warpage after ejection. Small setting changes matter.
Measure fixed locations at the neck, shoulder, body, and base. Check every cavity. Use ultrasonic readings for quick screening, then verify selected parts by sectioning and measuring.
Check at least three parts per cavity when possible. Record cavity number, cycle, resin lot, and machine settings. One attractive sample proves very little.
Map thin and thick zones against gate position and cooling layout. Use color maps to show trends. A stable average can hide a corner only two millimeters wide.
Calibrate instruments before the study. Measure warm and cooled parts separately. Change one process variable at a time. I would not trust clean-looking data without checking sampling quality.
Achieving consistent packaging quality begins with understanding the causes of wall thickness variation, including uneven cooling, unbalanced material flow, improper gate placement, shrinkage, and inconsistent mold alignment. To learn how to ensure wall thickness uniformity in packaging molds, designers should develop balanced cavity geometry, maintain suitable draft angles, optimize transitions, and position gates and cooling channels to support even filling and heat removal. Mold materials and polymer selection should also match the product’s shape, required strength, and processing conditions.
During production, stable control of melt temperature, injection speed, pressure, holding time, cooling time, and cycle consistency is essential. Regular inspection through dimensional measurements, section analysis, and statistical quality data can reveal thin or thick areas before they become major defects. By connecting inspection results with mold adjustments and process optimization, manufacturers can steadily improve uniformity, reduce material waste, and produce reliable packaging with consistent performance.

Ohio Machine