Flash is one of the clearest signs that an injection molding process is losing control. It appears as a thin, unwanted edge around the parting line, ejector pins, vents, or inserts. In 2026, manufacturers face tighter tolerances, recycled materials, faster cycles, and stronger pressure to reduce waste. These demands make flash prevention more important than simple trimming.
John Bozzelli, founder of Scientific Molding, offers a useful warning: “If you don’t know what is happening in the mold, you are just guessing.” His point applies directly to how to reduce flash in plastic injection molding. Flash usually reflects a mismatch between clamp force, injection pressure, mold condition, material behavior, or process settings. Increasing clamp tonnage may hide the symptom, but it may not correct the cause.
Look closely at the mold. A worn parting line can feel sharp under a fingertip. A blocked vent may leave a dark burn mark beside the flash. Excessive melt temperature can make the material flow too easily into small clearances. Mold alignment, platen parallelism, and insert seating also deserve measurement, not assumptions.
A reliable approach begins with evidence. Record pressure, temperature, shot size, cushion, and cycle time. Then change one variable at a time. Sometimes the real problem is not the machine. It is poor maintenance or an inaccurate process window.
Mistakes happen.
This guide examines practical inspection methods, scientific molding principles, material considerations, and maintenance strategies. It also recognizes an uncomfortable truth: some flash cannot be eliminated through settings alone. The mold may need repair, redesign, or replacement.
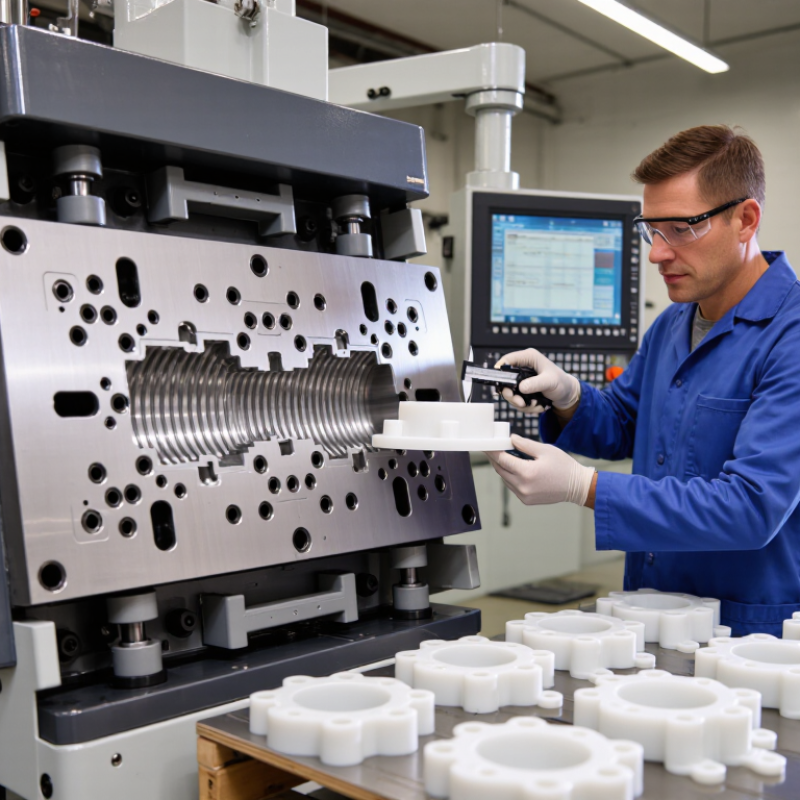
Flash in plastic injection molding should be judged by function, not appearance alone. ISO 20457 provides tolerance principles for molded parts, but it does not create one universal flash limit. The drawing, material, part size, and functional surface must guide acceptance. A visible edge may be harmless, while a smaller burr can block assembly or cut a sealing lip.
Use a calibrated 0.02 mm gauge during inspection. Clean the part first. Place the gauge across the parting line without forcing it. If the gauge enters the flash or passes through a gap, record the location and measured condition. Check several parts from the same batch. Flash often varies near corners, ejector marks, and uneven mold contact.
Our early inspections relied too heavily on photographs. That was a mistake. Lighting made thin flash appear worse, while soft flash sometimes disappeared completely. A gauge creates a more repeatable decision, but it is not perfect. Temperature, gauge wear, and operator pressure can affect the result. Inspectors should record these factors beside the measurement.
Set the acceptance rule on the drawing or inspection plan. For example, a 0.02 mm gauge may identify a critical flash condition, while a functional test confirms its real impact. Review mold alignment, clamping force, venting, and parting-surface damage after repeated failures. Do not remove flash blindly. Excess trimming can damage the sealing edge and hide the original molding problem.
Practical flash-severity screening framework for injection-molded parts. Compare the measured flash with the drawing tolerance assigned under ISO 20457, then confirm the edge condition with a calibrated 0.02 mm gauge.
| Flash Severity | Measured Flash Height | 0.02 mm Gauge Check | ISO 20457-Based Disposition | Typical Process Indicators | Recommended Corrective Action |
|---|---|---|---|---|---|
| Level 0 | Not visible at 10× magnification; typically below 0.01 mm. | Gauge does not enter the parting-line edge or functional gap. | Accept when the feature remains within the specified drawing tolerance and does not affect fit, sealing, appearance, or safety. | Stable mold clamping, clean parting surfaces, consistent melt filling, and balanced cavity pressure. | Continue process monitoring. Record mold-parting-line cleanliness and verify dimensions at the defined sampling frequency. |
| Level 1 | 0.01–0.02 mm; visible only under magnification. | A 0.02 mm gauge cannot pass through the flash or functional interface. | Generally acceptable only if the assigned ISO 20457 tolerance is not exceeded and the customer drawing permits the edge condition. | Minor wear, small venting variation, slight overpacking, or a small amount of contamination on the parting line. | Clean and inspect the parting line, check clamp force and injection peak pressure, and trend flash height before making tooling changes. |
| Level 2 | 0.02–0.05 mm; clearly visible along a limited area. | Gauge contacts the flash or passes locally at the edge. | Conditional acceptance only after dimensional inspection confirms compliance with the applicable ISO 20457 tolerance class and drawing requirements. | Insufficient mold shut-off, excessive injection pressure, excessive packing time, uneven mold temperature, or localized vent blockage. | Reduce peak injection or holding pressure in controlled steps, optimize holding time, clean vents, inspect shut-off surfaces, and verify mold alignment. |
| Level 3 | 0.05–0.10 mm; continuous flash or flash extending around a functional feature. | A 0.02 mm gauge passes through the flash or the flash interferes with fit or sealing. | Reject unless a documented engineering review confirms that the flash remains outside all functional and dimensional requirements. | Parting-line damage, inadequate clamping force, mold deflection, excessive cavity pressure, or severe venting restriction. | Stop release of affected parts. Repair or rework the parting surface, check platen parallelism and clamp force, restore vent depth, and revalidate the process. |
| Level 4 | Above 0.10 mm, sharp flash, torn flash, or flash affecting assembly, sealing, safety, or appearance. | Gauge passes freely, or the edge creates a sharp projection or prevents assembly. | Nonconforming condition. ISO 20457 dimensional compliance cannot override a functional, safety, or customer-specific rejection criterion. | Major mold mismatch, broken shut-off, mold opening under pressure, incorrect clamp setup, or uncontrolled injection and packing conditions. | Quarantine parts immediately. Correct the mold and machine setup, identify the root cause using pressure and dimensional data, then complete first-article and process-capability verification. |
Measurement note: ISO 20457 acceptance depends on the nominal dimension, tolerance class, material behavior, part geometry, and the applicable product drawing. The 0.02 mm gauge is a practical screening tool, not a replacement for calibrated dimensional measurement or the specified ISO 20457 tolerance. Gauge condition, contact force, measurement direction, and operator technique should be standardized.
No. Acceptance depends on function, drawing requirements, material, and part size. A visible edge may not affect assembly. A smaller burr can damage a sealing lip.
Use a calibrated 0.02 mm gauge. Clean the part before inspection. Place the gauge across the parting line without forcing it. Record the location if the gauge enters the flash or gap.
Check several parts from the same production batch. Flash can vary near corners, ejector marks, and uneven mold contact. Use several parts. One sample can mislead you.
Photographs alone are unreliable. Lighting may exaggerate thin flash or hide soft flash. A gauge gives better repeatability, but it is not perfect. Temperature, gauge wear, and operator pressure can change results.
Put the rule on the drawing or inspection plan. The tolerance standard provides principles, not one universal flash limit. A functional test should confirm whether the flash creates a real problem.
Reduce injection speed near the end of filling. Keep enough speed to prevent premature freezing. Control pressure so the cavity fills without slightly opening the mold. Small pressure changes can matter.
A practical starting point is 95–98% cavity fill. Verify part weight and appearance afterward. Holding pressure should build gradually around thin walls. This range needs adjustment for the actual mold.
Keep a stable melt cushion around 3–6 mm. Too little cushion can make transfer inconsistent. Too much may increase residence time and pressure variation. It is only a starting range.
Review the last 10 shots before making adjustments. Check clamp force, vent condition, melt temperature, shot size, and mold temperature. Change one factor at a time. Some failures require mold repair, not more tuning.
Reducing molding flash starts with defining an objective acceptance standard. This guide explains how to reduce flash in plastic injection molding by evaluating flash severity against ISO 20457 tolerances and using a 0.02 mm gauge for practical inspection. Careful examination of the parting line, mold shutoff surfaces, and alignment features is essential, with shutoff gaps maintained below 0.02 mm wherever possible. Correct clamp force is also critical and should generally be calculated at 2–5 tons per square inch of projected part area to prevent mold opening during filling.
Process settings must then be balanced rather than adjusted randomly. Injection speed, pressure, and the V/P switchover point should be tuned to control filling and packing without overloading the cavity. Maintaining a stable 3–6 mm melt cushion can improve repeatability. Finally, validate the settings by producing 30–50 consecutive parts, monitoring key dimensions with SPC, and targeting a Ppk of at least 1.33. This structured approach helps reduce defects, stabilize production, and support consistent part quality.

 Ohio Machine